Hey there, let’s cut to the chase – if you’re working with ASTM/ASME HSLA steel plate and drilling holes in it, the quality of those holes isn’t just a “nice-to-have” detail. Trust me, I’ve been supplying these plates for almost a decade, and I’ve seen way too many projects go sideways because someone skipped over the hole specs. HSLA (high-strength low-alloy) is tough stuff – that’s why you reach for it for bridges, heavy equipment, pressure vessels, all that industrial work – but its strength also makes drilling tricky. Mess up the hole, and you’re looking at fastener failure, structural weak points, or even a whole part getting tossed. Let’s break down exactly what hole quality requirements you need to hit here, no stuffy industry jargon (well, the necessary stuff, at least) and real-world context from someone who’s lived this. ASTM/ASME HSLA Steel Plate
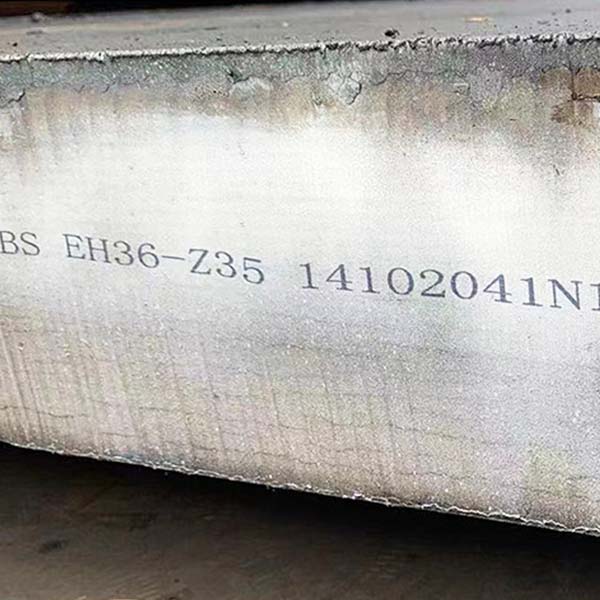
First off, let’s make sure we’re on the same page: HSLA plate is different from regular carbon steel. It’s got that added alloy mix (think niobium, vanadium, titanium) that gives it higher tensile strength without weighing it down, but those same elements can make the material more abrasive when you drill. That’s why your hole quality can’t be the same as what you’d use for a basic mild steel bracket. Let’s start with the big one every inspector and project manager cares about: dimensional accuracy. If your hole is too big or too small, you can’t get a tight fit for bolts, rivets, or whatever fastener you’re using. For ASTM/ASME HSLA, the standard hole tolerance isn’t just a random number – it’s spelled out specifically for these steels, because their strength means even a tiny oversize hole can create stress concentrations. The general rule we follow for most HSLA grades (like A572 Grade 50, A606, or A709) is that a standard drilled hole’s diameter has to stay within +0.005 inches and -0.000 inches of the nominal size. Wait, let me be clear – that’s not a “give or take” like you see with some casual fabrication. If you’re using a 1-inch hole, it can’t be 1.006 inches max, and it can’t be smaller than 1.000 inches. A smaller hole might sound like it’s better for a tight bolt fit, but HSLA’s hardness can cause the drill bit to wander, or even snap, when you’re drilling something that’s not just a little undersized. On the flip side, an oversize hole is a disaster for structural integrity – you’ll have to plug and re-drill, which introduces a new weak point, or use an oversized bolt that might not meet the grade specs for HSLA parts.
Then there’s hole location, and this is where so many fabricators cut corners. If your hole is off by even a sixteenth of an inch from where it’s supposed to be, when you line up two HSLA plates for a bridge connection or a crane arm, those holes won’t align. For ASTM/ASME applications, the positional tolerance for drilled holes is usually within ±0.010 inches relative to the layout marks. That means if your drawing says a hole is 6 inches from the edge and 4 inches from another hole, it can’t be 5.985 inches from the edge or 4.015 inches from the other hole. I’ve had customers call me panicking because they drilled a set of A572 Grade 50 plates and the holes were 0.020 inches off – they had to send the whole stack back, which cost them time and money, and it all could’ve been avoided with a quick check of the location tolerance. HSLA plates have a tighter grain structure than mild steel, so drill wander is a real risk if you don’t use the right tooling, but even with good tools, if your layout is off or your drill press isn’t calibrated, you’re going to run into location issues that make the whole part unusable.
Next up, surface quality of the hole wall – this is the one that people overlook until it’s too late. HSLA’s abrasive nature means that if you use a dull drill bit, or the wrong cutting speed, you’ll get a rough hole surface. That rough surface isn’t just ugly; it creates stress risers, which are exactly where cracks start in high-load applications. For ASTM/ASME HSLA, the maximum allowable surface roughness (Ra) for drilled hole walls is typically 250 microinches, but for critical applications (like pressure vessels or seismic bridge joints), that drops to 125 microinches. What does that actually mean? A Ra of 250 is like the roughness of fine sandpaper, and 125 is smoother, like a standard printer paper. If you see any built-up edge on the drill bit, or smearing along the hole wall, that’s a sign you’ve exceeded that roughness limit. I always tell my customers: if you can run your finger along the hole wall and feel a distinct ridge or rough spot, that’s too rough. We’ve had a customer have a crane arm fail in testing because they skipped smoothing the rough drilled holes – the cracks started exactly where the surface was roughest, and it all traced back to drilling at too slow a speed with a worn bit. HSLA works hard, so its holes need to be smooth to keep up.
Wait, let’s talk about hole type – not all drilled holes are the same, and ASTM/ASME has specific rules for that too. If you’re drilling a standard clearance hole for a bolt, that’s straightforward, but if you need a countersink or counterbore for a hex head bolt or socket head cap screw, those have their own requirements. The countersink angle has to be within 1 degree of the specified angle, and the depth can’t be more than the thickness of the bolt head – if it’s too deep, you weaken the plate’s edge, if it’s too shallow, the bolt won’t seat properly. For HSLA, which has higher yield strength than mild steel, a bolt that doesn’t seat right means the load isn’t distributed evenly across the plate, leading to premature failure. I also should mention anything about burrs here – those sharp metal flakes left on the hole edges after drilling. ASTM/ASME standards say you have to remove burrs that are taller than 0.005 inches, especially on the outer edges of the plate. Burrs might seem tiny, but when you’re tightening a bolt, that burr can get sheared off, create a groove in the bolt shank, or even catch on other parts during assembly. We once shipped a load of A709 HSLA plate for a highway bridge, and the fabricator didn’t deburr the holes – during assembly, a burr got knocked loose and fell into a support beam, causing a minor delay that could’ve been fixed with a quick deburr step.
Now, let’s get into some material-specific stuff that’s unique to HSLA. Unlike carbon steel, some HSLA grades (like those with higher copper or chromium content) can be prone to work hardening when drilled at the wrong parameters. If you run the drill too slow, the heat and friction will make the hole edge harder, which can cause the next hole you drill to have inconsistent quality, or even damage the drill bit. That’s why we always recommend that our customers use high-speed steel (HSS) or carbide drill bits when drilling HSLA – carbide holds an edge longer, which keeps the hole smooth and dimensional. Also, the drill speed: for most HSLA grades, you want a cutting speed of around 70 to 100 surface feet per minute (SFPM) for carbide bits, compared to 100 to 150 for mild steel. Too fast, and you get burning on the hole wall, which ruins the surface quality; too slow, and you get work hardening and burrs. It’s a fine balance, but it’s non-negotiable for meeting the hole quality requirements.
Another thing that’s often missed: hole cleanliness. ASTM/ASME applications, especially for pressure vessels or food-grade equipment (yes, some HSLA grades are used for that), require holes to be free of metal shavings, dust, or any other debris. Those shavings can get caught between the fastener and the plate, leading to uneven load distribution, or cause corrosion over time. When we process our HSLA plates at the warehouse, we blow out all drilled holes with compressed air before shipping, and we recommend our customers do a visual check and a quick wipe with a clean cloth after drilling to make sure there’s no leftover debris. I can’t tell you how many times a customer has come back saying a fastener didn’t fit right, and it was just a tiny shaving stuck in the hole.
Wait, let’s also cover how these requirements are verified, because that’s part of the quality process. You can drill a perfect hole, but you have to prove it meets the specs. For dimensional accuracy, you’ll use a micrometer or a coordinate measuring machine (CMM) to check the diameter and location. For surface roughness, a profilometer is the go-to tool, though some fabricators use a rough comparator chart for quick checks, which works for less critical jobs. Burr height is easy with a feeler gauge – run it along the hole edge, and if it catches, it’s too high. Most third-party inspectors that work with ASTM/ASME projects will require these checks, so you can’t skip them. I always advise my customers to do 100% inspection on critical parts, and at least a sample inspection (10% of holes) on non-critical, that way you catch issues early before the whole part is finished.
Let’s address a common myth I hear all the time: “I can just ream a drilled hole to fix it if it’s off.” Yeah, you can ream, but that doesn’t fix bad hole quality, and it can mess up the dimensional tolerance. Reaming is supposed to be a finishing step for precision holes, not a fix for a bad drilled hole. If your drilled hole is already oversize because of wander or a dull bit, reaming it will make it even bigger, which is worse for stress concentrations. And if the original hole wall was rough, reaming will smooth it out, but it won’t fix any work hardening or stress from drilling. So don’t think of reaming as a cure-all – it’s a complement to good drilling practices, not a replacement.
Now, why does all this matter for HSLA specifically? Let’s circle back to the material’s purpose. HSLA is used in applications where failure isn’t an option – bridges that carry thousands of cars a day, cranes lifting 50-ton loads, pressure vessels holding high-pressure gas. Those holes are part of the load path, so any weakness in the hole directly weakens the whole structure. I’ve seen mild steel plates get away with slightly loose hole tolerances because their lower strength means they handle stress better, but HSLA? Not so much. The ASTM/ASME standards are written for these exact scenarios, to make sure the material’s high strength isn’t wasted by bad hole quality.
At the end of the day, the key takeaway here is that hole quality for ASTM/ASME HSLA steel plate isn’t arbitrary. Every requirement – dimensional tolerance, location, surface roughness, burr removal, cleanliness – is there to make sure the plate performs as intended, no matter how much load it’s under. I’ve spent years talking to fabricators, engineers, and contractors about this, and the number one mistake I see is treating HSLA like it’s just another type of steel. It’s tougher, but drilling it requires attention to detail and sticking to those specs.
If you’re working on a project that needs ASTM/ASME HSLA plate, and you want to make sure you get the right material that plays nice with good hole drilling, don’t hesitate to reach out. We can help you pick the right HSLA grade for your application, share our own drilling best practices we’ve learned over the years, and make sure you get plate that meets all the necessary standards so your hole drilling goes as smooth as possible. No stress, no hidden hoops, just honest advice from someone who’s been in the game for a long time.
ASTM/ASME HSLA Steel Plate References:
- ASTM A6/A6M-21, Standard Specification for General Requirements for Rolled Structural Steel Bars, Plates, Shapes, and Sheet Piling
- ASME BPVC Section VIII, Division 1, Rules for Construction of Pressure Vessels
- Oberg, E., Jones, F.D., Horton, H.L., & Ryffel, H.H. (2016). Machinery’s Handbook (31st ed.). Industrial Press.
- AWS D1.1/D1.1M-20, Structural Welding Code – Steel
Gnee Steel (Tianjin) Co., Ltd.
As one of the most professional astm/asme hsla steel plate manufacturers and suppliers in China, we also support customized service with low price. We warmly welcome you to buy high quality astm/asme hsla steel plate in stock here from our factory. If you have any enquiry about free sample, please feel free to email us.
Address: No.4-1114, Beichen Building, Beicang Town, Beichen District, Tianjin, China
E-mail: alloy@gneesteelgroup.com
WebSite: https://www.chinavesselplates.com/
